Laser cutter kerf settings · A workshop guide
Get the
fit right.
Loose joints, tight slots, and the small amount of material your laser removes. Set up a test before committing a whole sheet.
Published
Updated
01 / The cut itself
A line in the file.
A gap in the wood.
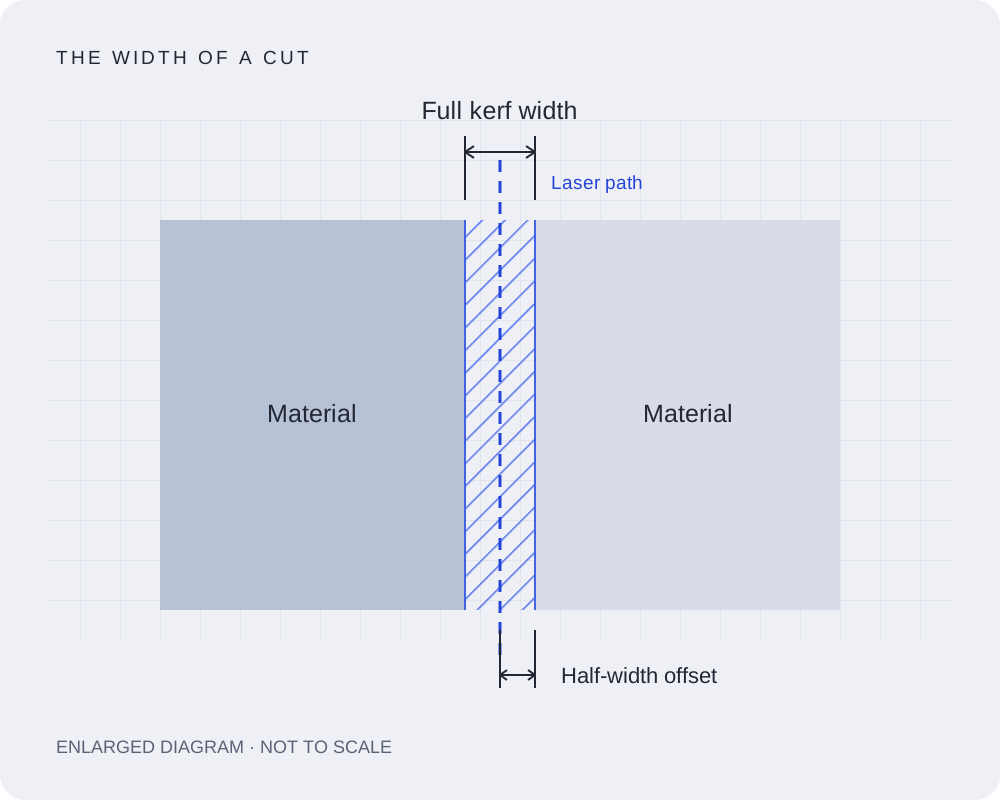
When you cut a wooden model, the laser removes a narrow strip of material along each line. That strip’s width is the kerf. Cut along the centre of an outline without compensation and you get a slightly smaller part. An internal slot becomes wider.
On a decorative silhouette, you might barely notice. On a model with dozens of interlocking parts, that difference affects how the whole assembly holds together.
Kerf compensation moves the cutting path towards the material you will discard, keeping more of the edge you need. The starting offset is half the measured cut width. You still need a joint test to find the fit you want.
- Full cut width
- 0.20 mmThe entire strip removed by the beam
- Path offset
- 0.10 mmHalf the width, on each boundary
Illustrative numbers, not recommended settings for your machine. LightBurn’s worked example explains the half-width calculation.
02 / Before the full sheet
Start with a small joint.
I use a small fit test before cutting a full model. It gives you something to hold and assemble, so you can judge the result without discovering a problem halfway through a build.
Measure your material.
Check the sheet with calipers in several places. Plywood sold as 3 mm may not measure exactly 3 mm. Choose a file version or scale that suits the actual thickness before tuning the kerf.
Use the conditions for your project.
Cut a test from the same material with the focus, power, speed and number of passes you intend to use. First get a clean cut all the way through. Then assess the joint.
Make one change at a time.
Keep the cutting conditions fixed while you adjust compensation. Fit the pieces together by hand, note the value, and cut another test if needed. Stop if you have to force a delicate part.
My Laser Cut and Engraving Test File on MakerWorld includes fit-test blocks at the top and line/fill engraving tests below. Use the top section for this guide. The listed laser profile is for 3 mm birch plywood; check your material before using its setup.
Thickness and kerf need separate checks. Scaling a design changes its slots, tabs and overall dimensions together. Kerf compensation adjusts its cut edges. Don’t use a large kerf value to make a file for the wrong material thickness fit.
03 / In LightBurn
Adjust the cutting layer.
Put your test parts on a Line layer and double-click that layer in the Cuts / Layers window. Find Kerf Offset in the Cut Settings Editor. If the option is hidden, check whether Beginner Mode is enabled.
A positive value moves outer paths outward. LightBurn reverses the direction for holes enclosed by other shapes on the same layer. The setting works with closed paths; check your artwork if a contour does not respond.
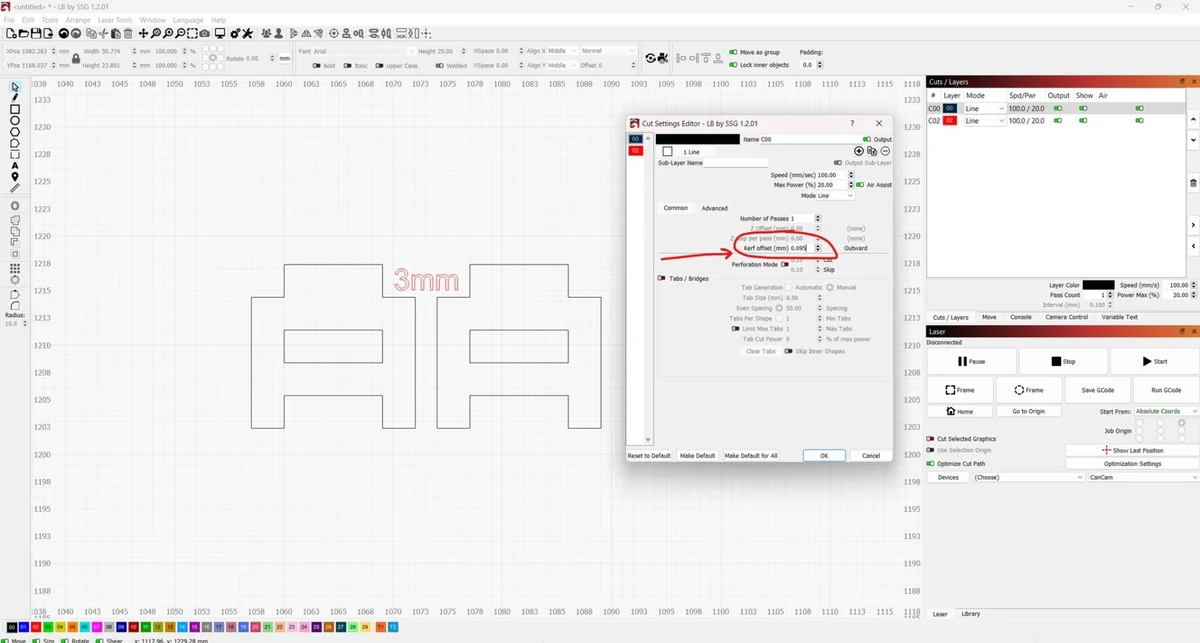
If you need to measure kerf first, LightBurn provides a Vernier test and instructions. Follow that test with compensation set to zero, then use its calculated offset in the layer settings.
Open Preview to inspect the compensated paths. LightBurn applies the offset when generating the cut, so the drawing itself does not change. Leave space between parts and cut a small joint before running the full sheet.
Reference: LightBurn’s Kerf Offset settings.
04 / Prepare the SVG
You can use Laser Studio, too.
I’m building Laser Studio to prepare SVG files for cutting. You can adjust their scale, apply kerf compensation, add holding tabs and arrange parts before exporting.
For a tour of the editor with screenshots, see the Laser Studio walkthrough.
Import your original SVG and check which colours are assigned to Cut or engraving. Set the scale for your material first. Then apply kerf compensation to the closed cutting contours and compare the original and adjusted paths.
Outer paths move outward; hole paths move inward. Engraving and open cuts keep their paths. If Laser Studio flags an issue, inspect the highlighted contour and resolve it before exporting.
Apply compensation once. Laser Studio includes the adjustment in the exported SVG. Set the additional kerf or cut offset in your laser software to zero when using that compensated file. Keep the original SVG so you can prepare it again for different material.
Laser Studio is free to use, with no sign-in required. This workflow uses SVG files; check the available formats when downloading a project.
05 / Read the result
Let the test pieces tell you.
For a correctly scaled joint, increasing positive compensation leaves more material at the mating edges and makes the fit tighter. Reduce it for a looser fit. Make small changes and compare a fresh cut each time.
- The joint is loose.
- Check that the material matches the file, then increase positive compensation a little. Confirm that the setting applies to the intended closed cut paths.
- The joint is too tight.
- Check the sheet thickness and scale. Reduce compensation, and make sure you haven’t applied it both in the SVG and in the laser software.
- Some joints fit, others don’t.
- Check thickness variation, cut quality and part orientation. Some diode beams have different kerf widths along the two axes, so one number may not suit both directions equally.
I keep a note of the material, measured thickness, cutting settings and offset beside each test. It is easy to forget which tiny adjustment produced the fit you liked.
A good result is a joint you can assemble without damage, with the amount of friction the model needs. Recheck it when you change material or cutting conditions. On a large build such as Big Boy, that small test is worth doing before hundreds of parts reach the bench.
From your workshop
Join the conversation.
Share what worked for you, or leave a question about the guide.
Local preview: comments are saved on this computer.
Loading comments…